Swiss-Type Lathe for the Americas: How to Solve Precision Small-Part Manufacturing Challenges
Manufacturing companies across the Americas are under increasing pressure to produce more efficiently while maintaining consistent quality.
Customers expect shorter delivery times, stable product quality, competitive pricing, and reliable supply. At the same time, manufacturers must manage labor costs, skilled-worker shortages, material costs, equipment investment, and increasingly complex production requirements.
These challenges become particularly important when manufacturers produce small, long, slender, or precision-critical components.
A component may appear relatively simple on a technical drawing, but producing thousands or even millions of identical parts with stable dimensions can be much more difficult than producing a small batch.
Problems such as workpiece deflection, vibration, dimensional variation, poor surface finish, repeated setup, secondary machining, and manual handling can gradually increase the cost of every finished component.
This is where a Swiss-type lathe can provide a significant manufacturing advantage.
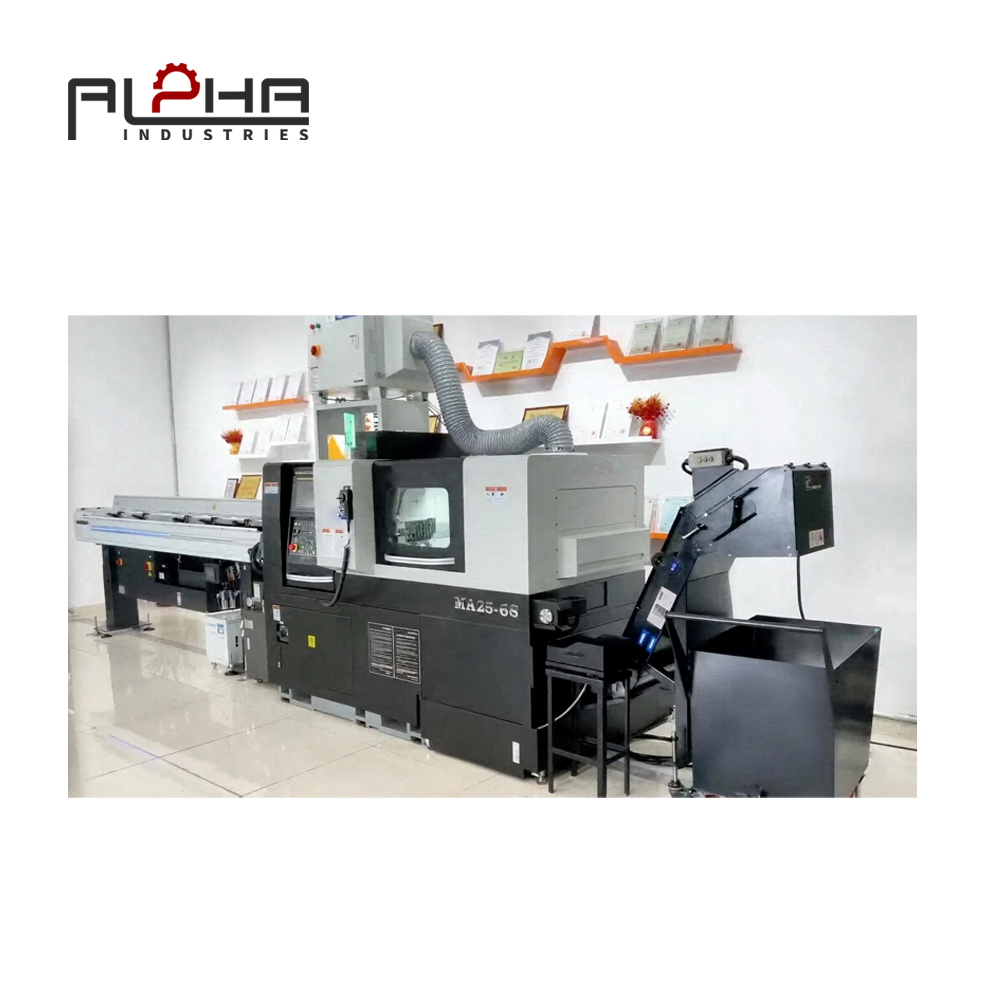
A Swiss-type lathe, also known as a sliding-headstock lathe or Swiss turning machine, is designed specifically for machining small and precision components. Unlike a conventional turning machine that primarily supports the workpiece from the chuck or collet, a Swiss-type lathe uses a guide bushing to support the bar close to the cutting area.
This basic design principle makes Swiss-type turning particularly suitable for long and slender workpieces.
For manufacturers in North America, Central America, and South America, the real question is therefore not simply whether a Swiss-type lathe is more advanced than a conventional lathe.
The more important question is:
Can a Swiss-type lathe solve the production problems that are currently increasing your manufacturing cost?
Why Small and Slender Parts Are Difficult to Machine
Small precision components can create unique machining challenges.
When a workpiece has a small diameter and relatively long machining length, the unsupported portion of the material can become susceptible to cutting forces.
During turning, the cutting tool applies force to the workpiece. If the workpiece is not sufficiently supported, it can deflect or vibrate.
Even a small amount of movement can affect the final component.
This may result in:
-
Dimensional variation
-
Taper
-
Chatter marks
-
Poor surface finish
-
Inconsistent diameter
-
Reduced concentricity
-
Additional inspection requirements
-
Higher scrap rates
-
Increased production costs
The problem becomes more significant when manufacturers need to produce large quantities of identical components.
Producing one acceptable part is different from producing tens of thousands of parts with the same dimensional accuracy.
This is one of the main reasons why Swiss-type machining has become an important solution for precision small-part manufacturing.
How the Guide Bushing Improves Machining Stability
The guide bushing is one of the defining features of a Swiss-type lathe.
During machining, the bar passes through the guide bushing, which supports the material close to the cutting area.
This significantly reduces the unsupported length of the workpiece during the machining process.
The result is improved control over workpiece movement.
For long and slender components, this can help reduce:
-
Deflection
-
Vibration
-
Chatter
-
Dimensional instability
-
Surface-finish problems
The importance of the guide bushing becomes particularly obvious when comparing the machining of a short, thick component with a long, thin shaft.
A short and rigid workpiece may not require specialized support.
A long and slender workpiece can behave very differently.
This is why manufacturers should evaluate the length-to-diameter ratio of their components when deciding whether Swiss-type machining is appropriate.
The guide-bushing system is not simply an additional machine feature. It is a fundamental part of the machining strategy.
The Labor Challenge Facing Manufacturers in the Americas
Labor efficiency is becoming an increasingly important consideration for manufacturers.
The cost of purchasing a machine is only one part of the total manufacturing cost.
Manufacturers also need to consider:
-
Operator requirements
-
Setup time
-
Material handling
-
Workpiece transfer
-
Inspection
-
Secondary machining
-
Production downtime
-
Tool changes
-
Rework
-
Scrap
A machine that can reduce unnecessary manual operations can potentially improve the overall economics of production.
Swiss-type lathes can be configured with automated bar feeders and multiple machining tools.
Depending on the machine configuration, a single production cycle can include operations such as turning, facing, drilling, threading, grooving, milling, and parting.
Some configurations can also perform back-end machining with a sub-spindle.
This means manufacturers may be able to reduce the number of times a component must be removed, repositioned, and clamped.
Instead of moving a component between several machines, more operations can potentially be completed within a single automated process.
This can reduce manual handling and improve production consistency.
Reducing Secondary Operations Through Swiss Turning
Secondary operations can become a hidden manufacturing cost.
A component may initially require turning on one machine, drilling on another machine, threading in another process, and then additional finishing or inspection.
Every additional operation creates another opportunity for:
-
Setup errors
-
Positioning variation
-
Handling damage
-
Production delays
-
Additional labor
-
Increased work-in-process inventory
Swiss-type machining can consolidate multiple operations when the machine is properly configured.
For example, a small precision shaft may require external turning, grooving, threading, drilling, and back-end machining.
A properly configured Swiss-type lathe may perform many of these operations within the same automated production cycle.
This does not mean that every component should be manufactured on a Swiss lathe.
Instead, manufacturers should examine the complete production process.
The most important question is:
How many separate operations can be eliminated or consolidated?
This is often more useful than simply comparing the purchase price of different machines.
Why Automation Matters for High-Volume Production
For manufacturers producing large quantities of small components, automation can have a major impact on production efficiency.
A Swiss-type lathe can work together with automatic bar feeding systems to provide a continuous supply of raw material.
Once the machining program, tooling, cutting conditions, and process parameters have been properly established, the machine can repeatedly produce components with limited operator intervention.
This can help manufacturers improve:
-
Machine utilization
-
Production consistency
-
Labor efficiency
-
Production capacity
-
Cycle-time control
Automation is particularly valuable when the same or similar components must be manufactured repeatedly.
For example, a manufacturer producing thousands of connector pins, precision shafts, medical components, or hydraulic parts may benefit more from automated Swiss turning than a company producing only a few large components each day.
The business case should therefore consider annual production volume rather than machine specifications alone.
Material Utilization and Production Cost
Material cost is another important consideration for precision machining.
When manufacturers work with aluminum, stainless steel, brass, titanium, nickel alloys, engineering plastics, or other valuable materials, the cost of raw material can have a significant impact on overall production economics.
Swiss-type lathes typically process bar stock through the guide-bushing system.
This provides excellent support for slender parts, but manufacturers should also evaluate the remaining bar length and material utilization.
For some short components, a non-guide-bushing configuration may provide advantages.
For long and slender components, however, guide-bushing support can be more important than minimizing the final bar remnant.
This creates an important balance between:
Machining stability and material utilization.
The best solution depends on the actual component geometry, material, production volume, and machining process.
Swiss-Type Lathe Applications in the Americas
Swiss-type turning is particularly suitable for industries that require high quantities of small and precision components.
Medical Component Manufacturing
Medical manufacturing often requires small components with controlled dimensions and repeatable quality.
Potential applications include:
-
Surgical components
-
Medical pins
-
Instrument components
-
Small shafts
-
Precision screws
-
Connectors
-
Implant-related components
For these applications, machining stability and repeatability can be extremely important.
Aerospace Component Manufacturing
The aerospace industry uses a wide range of small precision components.
Examples include:
-
Precision pins
-
Shafts
-
Fasteners
-
Connectors
-
Bushings
-
Sensor components
Swiss-type turning can be particularly useful when components combine small diameters with tight dimensional requirements.
Electronics and Electrical Components
Electronic products often contain large numbers of small precision components.
These may include:
-
Connector pins
-
Electrical terminals
-
Contacts
-
Sensor components
-
Precision shafts
-
Small housings
When production volumes are high, automated turning can help manufacturers maintain consistent production output.
Automotive Manufacturing
Automotive systems require many small machined components.
Swiss-type machining can be considered for applications involving:
-
Sensor components
-
Hydraulic components
-
Fuel-system parts
-
Precision shafts
-
Fasteners
-
Valve components
The ability to combine several machining operations can be particularly useful when manufacturers need to reduce handling between processes.
Hydraulic and Pneumatic Components
Hydraulic and pneumatic systems often use precision stems, fittings, pins, sleeves, and valve components.
These parts may require stable diameters, threads, grooves, and other detailed features.
Swiss-type machining can provide an efficient solution when the part geometry and production volume are suitable.
Swiss-Type Lathe vs. Conventional Lathe
There is no universal answer to whether a Swiss-type lathe is better than a conventional turning machine.
The right choice depends on the workpiece.
| Production Requirement | Swiss-Type Lathe | Conventional Lathe |
|---|---|---|
| Long slender components | Excellent | More challenging |
| Small-diameter components | Excellent | Application dependent |
| High-volume production | Excellent | Good |
| Multi-operation small parts | Excellent | May require additional processes |
| Automated bar feeding | Excellent | Available depending on configuration |
| Short thick components | May be unnecessary | Excellent |
| Heavy cutting | Application dependent | Often advantageous |
| Precision small parts | Excellent | Good depending on machine |
| Complex small components | Excellent | Application dependent |
| Simple turning work | May be excessive | Often economical |
A Swiss-type lathe should therefore not be selected simply because it offers more advanced technology.
The machine should be selected because its design solves a specific manufacturing problem.
When Is a Swiss-Type Lathe the Right Choice?
A Swiss-type lathe is worth considering when several characteristics appear together.
The component may have a small diameter, a relatively long machining length, and tight dimensional requirements.
Production volume may also be high enough to justify automation.
The component may require several machining operations that could potentially be completed within a single cycle.
In addition, manufacturers may want to reduce manual handling and improve production consistency.
A useful evaluation should consider:
-
Part diameter
-
Part length
-
Length-to-diameter ratio
-
Required tolerance
-
Surface finish
-
Material
-
Production volume
-
Cycle time
-
Number of machining operations
-
Tooling requirements
-
Automation requirements
-
Material utilization
This provides a much more accurate basis for machine selection than comparing machine prices alone.
What Should American Buyers Consider Before Purchasing?
When purchasing a Swiss-type lathe, manufacturers should look beyond the basic machine specification.
The first consideration should be the actual component.
Provide the machine supplier with detailed information about the part, including drawings, material, diameter, length, tolerance, production quantity, and required operations.
The supplier can then evaluate whether a Swiss-type configuration is appropriate.
Tooling should also be considered.
A machine capable of performing many operations is only useful if the tooling configuration can efficiently support the actual component.
Bar feeding is another important consideration.
For high-volume production, the relationship between the machine, bar feeder, material diameter, bar length, and production cycle should be evaluated together.
After-sales service should also be part of the purchasing decision.
For manufacturers in the Americas, technical support, spare parts availability, remote assistance, installation support, training, and response time can all influence the long-term value of the machine.
Swiss-Type Machining as a Long-Term Production Strategy
A Swiss-type lathe should not simply be viewed as another machine tool.
For the right application, it can become part of a broader automated production strategy.
The guide bushing provides workpiece support.
The sliding headstock provides an effective machining structure for slender components.
The tooling system allows multiple operations to be combined.
The bar feeder provides continuous material supply.
Automation reduces manual handling.
Together, these technologies can create a production process designed around repeatability, efficiency, and stable small-part manufacturing.
This is particularly relevant for manufacturers in the Americas that are looking to improve production efficiency while maintaining competitive manufacturing costs.
Frequently Asked Questions About Swiss-Type Lathes
What is a Swiss-type lathe?
A Swiss-type lathe is a precision turning machine designed primarily for small and slender components. Its sliding-headstock and guide-bushing design supports the workpiece close to the cutting area, helping reduce deflection and vibration during machining.
What is a Swiss-type lathe used for?
Swiss-type lathes are commonly used for small precision components such as shafts, pins, connectors, medical components, aerospace parts, electronic terminals, hydraulic components, and other high-volume turned parts.
Why does a Swiss-type lathe use a guide bushing?
The guide bushing supports the bar close to the cutting area. This helps reduce the unsupported length of the workpiece and improves machining stability when producing long, slender components.
Is a Swiss-type lathe more precise than a conventional lathe?
Not automatically. Precision depends on the machine, tooling, material, programming, cutting conditions, operator skills, and production process. Swiss-type machines have a structural advantage for many small and slender components because of their guide-bushing support.
Can a Swiss-type lathe perform milling?
Many modern Swiss-type machines can be equipped with live tooling for milling and other secondary machining operations. The exact capability depends on the machine configuration.
Can Swiss-type lathes reduce labor costs?
They can reduce manual handling and operator intervention, particularly when combined with automatic bar feeding and multi-operation machining. The actual labor savings depend on the part, production volume, automation level, and process design.
Is Swiss machining suitable for high-volume production?
Yes. Swiss-type lathes are particularly well suited to repetitive production of small precision components, especially when automatic bar feeding and multi-operation machining are used.
How do I know if my part needs a Swiss-type lathe?
Start by evaluating the part diameter, machining length, length-to-diameter ratio, tolerance requirements, material, annual production volume, and number of machining operations. Long, slender, precision-critical parts are often strong candidates for Swiss-type machining.
Why Choose ALPHA for Swiss-Type Lathe Solutions?
For manufacturers looking to improve small-part machining efficiency, ALPHA focuses on providing practical metalworking solutions based on individual production requirements.
A suitable Swiss-type lathe should be selected according to the actual application rather than simply the machine's technical specifications.
ALPHA can help manufacturers evaluate factors such as:
-
Component dimensions
-
Material
-
Production volume
-
Required tolerance
-
Machining operations
-
Tooling configuration
-
Automation requirements
-
Production efficiency
-
Long-term manufacturing needs
The objective is not simply to purchase a machine.
The objective is to build a more stable, efficient, and repeatable manufacturing process.
If your company is evaluating Swiss-type turning equipment for the American market, ALPHA can help you assess the application and identify a suitable machining solution.
Explore the ALPHA machine range and discuss your requirements with our team.
Contact Us
Are you looking for a reliable Swiss Type Lathe for precision small-part manufacturing?
Whether you need to machine long slender shafts, precision pins, connectors, medical components, aerospace parts, hydraulic components, or other small precision parts, ALPHA can help you evaluate the right turning solution based on your material, part dimensions, tolerance requirements, production volume, and machining process.
Our team can provide professional assistance with machine selection, configuration, machining requirements, and production solutions.
Contact ALPHA today to discuss your Swiss-type lathe requirements and find the right solution for your production needs.