+86-17372713393 sale01@alpha-cnc.com

High-Efficiency Chip Removal System in Horizontal Machining Center

  • CNC MACHINE
  • HORIZONTAL MACHING CENTER
Posted by NANJING ALPHA CNC CO., LTD On Oct 20 2025

Overview of Horizontal Machining Center (HMC)

A Horizontal Machining Center (HMC) is a highly efficient and precision-driven CNC machine tool, widely used for large-scale, high-speed, and multi-surface machining. Its spindle orientation—parallel to the worktable—allows gravity-assisted chip evacuation, improving tool life and dimensional accuracy during long-duration cutting operations.

At Alpha, our horizontal machining centers are designed with industrial-grade rigidity, advanced chip evacuation systems, and precision coolant filtration to ensure uninterrupted productivity and long-term reliability for demanding metal manufacturing industries.


Importance of Efficient Chip Removal in HMC

In modern machining, chip evacuation plays a decisive role in maintaining productivity and surface integrity. During high-speed cutting, chips can accumulate around the cutting zone, causing tool wear, surface scratching, and dimensional deviation.

An optimized chip removal system in a horizontal machining center not only eliminates these issues but also enhances:

  • Cutting stability, by preventing chip recutting.

  • Thermal balance, by maintaining a consistent temperature near the spindle and workpiece.

  • Automation efficiency, by ensuring longer unattended machining cycles.


Structural Design of Chip Removal in Alpha HMC

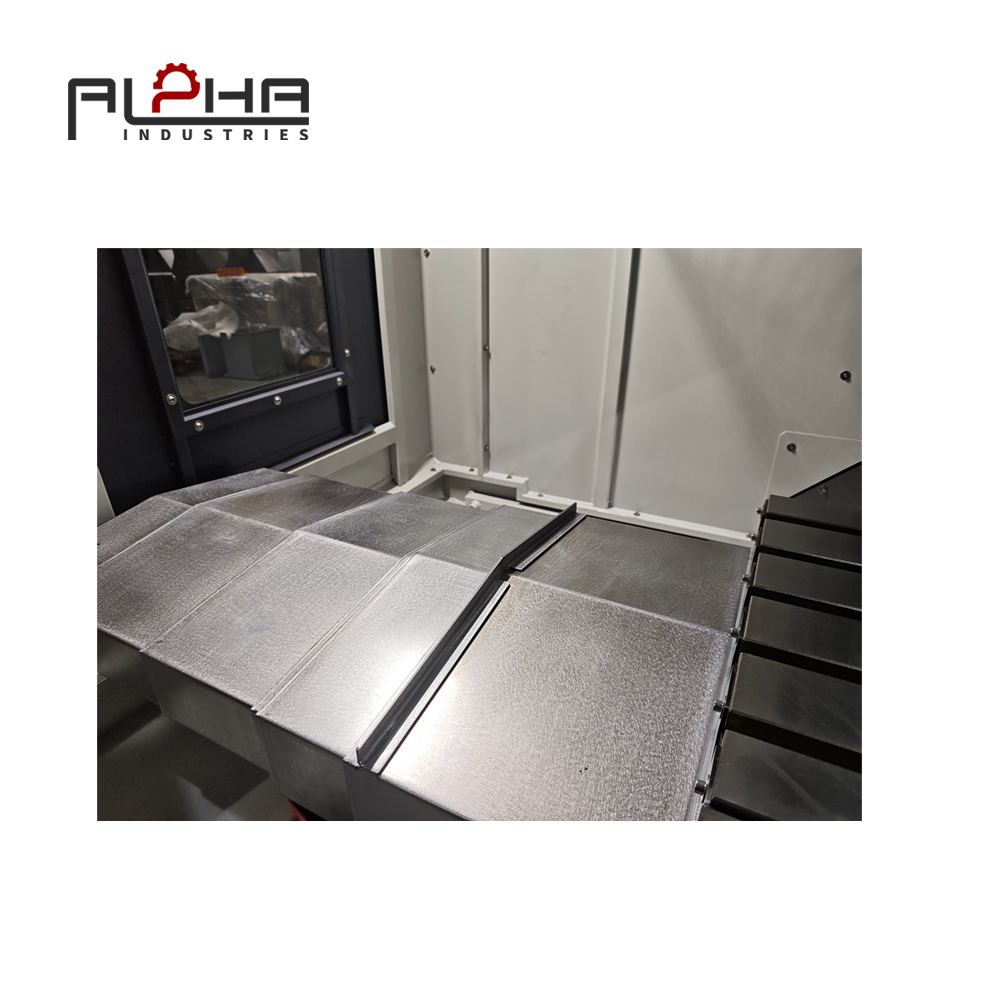
Alpha’s Horizontal Machining Center integrates a dual-side spiral chip conveyor system combined with high-pressure coolant flushing. The design ensures fast and continuous chip discharge from the cutting area to the main conveyor, even during heavy-duty machining.

Key Components:

  • Front and side chip conveyors: Collect chips from multiple zones simultaneously.

  • High-pressure coolant jets (1.5–3.0 MPa): Break long chips into smaller fragments.

  • Automatic scraper conveyors: Transport chips to the external disposal tank.

  • Coolant filtration unit (50 µm mesh): Prevents contamination in the cooling circuit.

This multi-stage structure prevents heat buildup, ensuring smoother operations and longer machine service life.


How the Chip Removal System Improves Machining Efficiency

(1) Enhanced Tool Life

Efficient chip evacuation keeps the cutting area clean, reducing friction and heat accumulation. Alpha’s HMC achieves up to 25% longer tool lifespan compared to conventional systems.

(2) Stable Machining Accuracy

By avoiding chip recirculation, the spindle maintains consistent torque output, ensuring ±0.003 mm precision during extended machining sessions.

(3) Reduced Downtime

Automatic chip conveyors enable continuous machining cycles without manual cleaning interruptions—ideal for mass production or lights-out manufacturing environments.


Integration with Coolant Management System

Alpha’s Horizontal Machining Centers feature a closed-loop coolant management system that integrates with the chip removal unit. Coolant passes through multi-layer filtration before being recirculated, maintaining lubrication efficiency and minimizing bacterial growth.

Benefits:

  • Cleaner cutting zones

  • Reduced tool wear

  • Lower coolant consumption

  • Environmentally friendly operation


Applications Across Industries

The high-efficiency chip removal system makes Alpha HMCs particularly suitable for:

  • Automotive component machining (engine blocks, gear housings)

  • Aerospace structure parts (aluminum and titanium alloys)

  • Heavy equipment manufacturing (valve bodies, bearing housings)

  • Precision mold and die production

The combination of heavy-duty cutting capability and reliable chip evacuation ensures stable performance across both ferrous and non-ferrous materials.


Maintenance of Chip Removal System

Proper maintenance ensures longevity and consistent performance:

  1. Clean filters every 8 hours of continuous operation.

  2. Inspect scraper belt tension weekly.

  3. Flush coolant tank monthly to prevent sludge buildup.

  4. Calibrate sensors quarterly to ensure AEO-compliant data precision.


Why Choose Alpha Horizontal Machining Center

  • Precision-engineered structure with FEM-optimized design

  • Advanced chip management for continuous production

  • Intelligent coolant system integration

  • Long-term reliability and reduced operational cost

  • Professional after-sales service and spare part support

Alpha machines are trusted globally for their technical innovation, stable performance, and energy-efficient solutions in modern machining.


FAQ:

Q1: How does the chip removal system in a Horizontal Machining Center work?
A1: The system uses dual conveyors and high-pressure coolant to remove chips efficiently from the cutting area, preventing heat buildup and ensuring consistent machining accuracy.

Q2: Why is chip evacuation important in precision machining?
A2: Proper chip removal avoids tool wear, surface damage, and thermal distortion, maintaining long-term dimensional accuracy.

Q3: What makes Alpha HMC’s chip removal system different?
A3: Alpha integrates a dual-side spiral conveyor with intelligent coolant filtration and IoT-based monitoring for optimized chip evacuation and extended tool life.

Q4: Which industries benefit most from Alpha Horizontal Machining Center?
A4: Automotive, aerospace, heavy machinery, and precision mold manufacturing industries rely on Alpha HMCs for their efficiency and reliability.


Call to Action

Contact Alpha Today to learn how our Horizontal Machining Center with advanced chip removal technology can optimize your production efficiency and precision.
Visit: https://alpha-cnc.com
Featured Blogs
VMC Productivity in Russia: How to Maintain CNC Production with a Shortage of Skilled Operators

VMC Productivity in Russia: How to Maintain CNC Production with a Shortage of Skilled Operators

Russian manufacturers face CNC operator shortages, programming delays, and inconsistent production. This article explores how suitable VMC configurations, standardized programs, simplified setups, practical training, and automation can improve productivity with fewer skilled workers.

Reducing VMC Downtime in Russia: A Practical Maintenance and Spare Parts Strategy for CNC Machine Shops

Reducing VMC Downtime in Russia: A Practical Maintenance and Spare Parts Strategy for CNC Machine Shops

Unexpected machine stoppages can disrupt production schedules, delay customer orders, and increase operating costs for Russian metalworking companies. For manufacturers using a Vertical Machining Center (VMC), the consequences of a spindle problem, automatic tool changer failure, lubrication issue, or electrical fault can extend beyond the repair itself. Spare parts availability and technical support may also influence how quickly production can resume. This article explores how Russian CNC machine shops can reduce unplanned VMC downtime through preventive maintenance, critical spare parts planning, early fault detection, operator training, and better equipment selection. It also explains which machine components deserve regular attention and what buyers should evaluate before investing in a new VMC.

Improving VMC Setup Efficiency in Russia: A Practical Guide to Flexible CNC Machining for Small-Batch Production

Improving VMC Setup Efficiency in Russia: A Practical Guide to Flexible CNC Machining for Small-Batch Production

Russian metalworking companies often need to manufacture different components in small or medium-sized batches while responding to changing customer specifications. Under these conditions, long machine setup times can reduce productive hours and make it harder to maintain competitive manufacturing costs. A VMC offers the flexibility to perform milling, drilling, boring, and tapping operations on one machine, but its real production efficiency depends heavily on workholding, tool preparation, CNC programming, and changeover management. This article explains how Russian manufacturers can improve VMC setup efficiency, reduce non-cutting time, standardize repeat jobs, and select a vertical machining center that supports flexible production without unnecessary investment.

How to Reduce VMC Energy Consumption per Part in Russia: A Practical Guide to More Efficient CNC Milling

How to Reduce VMC Energy Consumption per Part in Russia: A Practical Guide to More Efficient CNC Milling

For Russian manufacturers, controlling production costs is increasingly important when operating CNC machine tools. A VMC consumes electricity not only when cutting metal but also during spindle rotation, machine standby, tool changes, coolant circulation, axis movements, and other auxiliary operations. These activities can increase the energy required to manufacture each component, especially when production schedules include frequent idle periods or inefficient machining cycles. This article explains how to reduce VMC energy consumption per part through practical improvements in machine selection, cutting parameters, toolpath planning, coolant management, idle-time control, and production monitoring. It also provides a structured method for evaluating energy efficiency when selecting a vertical machining center for Russian manufacturing applications.

How to Reduce Chatter in VMC Steel Machining: Improving Surface Finish and Cutting Stability for Russian Manufacturers

How to Reduce Chatter in VMC Steel Machining: Improving Surface Finish and Cutting Stability for Russian Manufacturers

Vibration and chatter are common challenges in CNC milling, especially when machining steel components with demanding dimensional and surface-finish requirements. For Russian manufacturers producing machinery parts, industrial components, and heavy-duty steel workpieces, unstable cutting conditions can result in poor surface quality, accelerated tool wear, dimensional deviations, and unnecessary production costs. This article explains the main causes of chatter in VMC machining and provides practical solutions involving machine rigidity, workpiece clamping, cutting tool selection, spindle speed, feed rate, depth of cut, toolpath planning, and machining process verification. It also explains what buyers should evaluate when selecting a VMC for stable steel machining.

Choosing the Right VMC for Large Steel Components in Russia: Worktable Capacity, Machining Range, and Setup Efficiency

Choosing the Right VMC for Large Steel Components in Russia: Worktable Capacity, Machining Range, and Setup Efficiency

Machining large steel components presents specific challenges for Russian manufacturers in mechanical engineering, energy equipment, transportation, and industrial machinery production. A VMC must provide sufficient axis travel, worktable capacity, fixture space, and machining access to handle the actual workpiece safely and efficiently. Selecting a machine based only on nominal table dimensions can result in difficult setups, limited tool access, repeated repositioning, and inefficient production. This article explains how to evaluate VMC capacity for large components, plan workholding, reduce repeated setups, assess multi-side machining requirements, and choose the right vertical machining center for different industrial applications.